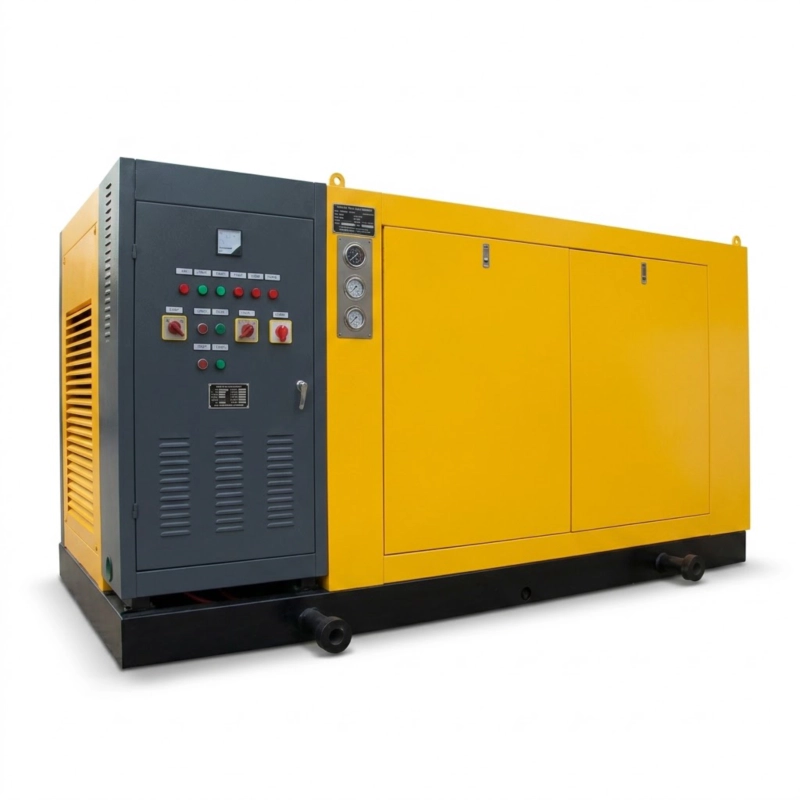
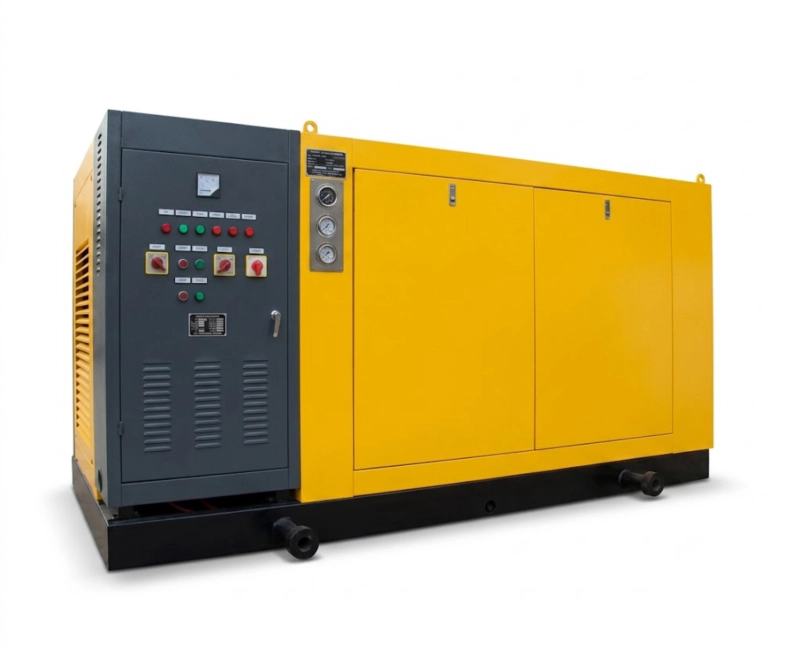
Product Overview: Screw Compressor for Industrial Compressed Air
The screw compressor is a twin-screw rotary positive-displacement machine designed for continuous compressed air supply in industrial facilities of all types and sizes. Unlike reciprocating piston compressors, the screw compressor has no inlet or discharge valves — compression is achieved by the meshing of a male and female helical rotor pair that progressively reduces the trapped gas volume as the rotors turn. This continuous rotary compression process produces a smooth, essentially pulsation-free compressed air output at constant pressure, with significantly lower vibration than a reciprocating compressor of equivalent capacity. It is the dominant technology for compressed air generation at 7.5–400 kW in modern industrial facilities for this reason.
Our screw compressor range covers 18 standard models from 7.5 kW to 400 kW, with free air delivery (FAD) from 0.8 m³/min to 65 m³/min at working pressures of 0.7 MPa, 0.8 MPa, 1.0 MPa, and 1.3 MPa. Each unit is supplied as a fully integrated package: the male and female rotors, oil-injection cooling system, integrated oil separator, air-cooled or water-cooled aftercooler, inlet filter, safety valve, pressure transducer, temperature sensors, and PLC controller are all mounted on a single baseframe, ready for connection to the plant compressed air network after installation. This integrated approach eliminates the on-site assembly, inter-component pipework, and instrumentation work that adds cost and commissioning time to bare compressor installations.
Variable frequency drive (VFD) models of the screw compressor regulate motor speed in response to the instantaneous air demand, reducing power consumption during periods of partial load by 20–35% compared with fixed-speed compressors that load and unload at full speed. In facilities with variable air demand — which describes the majority of manufacturing plants, fabrication shops, and food processing facilities — a VFD model reduces annual energy cost by a margin that commonly pays back the premium over fixed-speed models in 18–36 months. All models are GOST-R certified and available with full Russian-language documentation from our distribution network in Russia.
Technical Specifications — Screw Compressor Standard Range
Standard fixed-speed screw compressor models at 0.8 MPa working pressure. VFD models available for all power ratings; 1.0 MPa and 1.3 MPa pressure variants available on request. All units include integrated oil separator, aftercooler, inlet filter, and PLC controller.
| Model |
Motor (kW) |
FAD (m³/min) |
Pressure (MPa) |
Noise (dB(A)) |
Cooling |
Voltage |
| SC-7A |
7.5 |
0.8 |
0.80 |
≤65 |
Air |
380V |
| SC-11A |
11 |
1.2 |
0.80 |
≤65 |
Air |
380V |
| SC-15A |
15 |
1.8 |
0.80 |
≤66 |
Air |
380V |
| SC-22A |
22 |
2.8 |
0.80 |
≤66 |
Air |
380V |
| SC-30A |
30 |
3.6 |
0.80 |
≤68 |
Air |
380V |
| SC-37A |
37 |
4.8 |
0.80 |
≤68 |
Air |
380V |
| SC-45A |
45 |
5.8 |
0.80 |
≤70 |
Air |
380V |
| SC-55A |
55 |
7.2 |
0.80 |
≤70 |
Air |
380V |
| SC-75A |
75 |
9.5 |
0.80 |
≤72 |
Air / Water |
380V/6K |
| SC-90A |
90 |
11.5 |
0.80 |
≤72 |
Air / Water |
380V/6K |
| SC-110A |
110 |
14.0 |
0.80 |
≤74 |
Air / Water |
380V/6K |
| SC-132A |
132 |
17.0 |
0.80 |
≤74 |
Air / Water |
380V/6K |
| SC-160A |
160 |
21.0 |
0.80 |
≤75 |
Water |
380V/6K |
| SC-200A |
200 |
26.0 |
0.80 |
≤75 |
Water |
6K/10K |
| SC-250A |
250 |
33.0 |
0.80 |
≤76 |
Water |
6K/10K |
| SC-315A |
315 |
42.0 |
0.80 |
≤76 |
Water |
6K/10K |
| SC-400A |
400 |
65.0 |
0.80 |
≤78 |
Water |
6K/10K |
FAD rated at 0.80 MPa (8 bar), 20°C inlet, 101.3 kPa reference per ISO 1217. VFD variants available for all models — FAD range 40–100% of rated. 1.0 MPa and 1.3 MPa pressure variants available with adjusted FAD. Noise levels measured at 1 m in free field per ISO 2151. All units include integrated inlet filter, oil separator, aftercooler, safety valve, and PLC controller.
General Series Parameters — Screw Compressor
| Parameter |
Screw Compressor — Standard Range |
| Compression Principle |
Twin-screw rotary positive displacement; oil-injected cooling |
| Compressed Medium |
Atmospheric air; special gas variants on request |
| Working Pressure Options |
0.7 MPa (7 bar); 0.8 MPa (8 bar); 1.0 MPa (10 bar); 1.3 MPa (13 bar) |
| Free Air Delivery Range |
0.8–65.0 m³/min (ISO 1217 rated) |
| Drive Options |
Fixed-speed belt drive (7.5–55 kW); direct drive (75–400 kW); VFD available all ratings |
| Cooling System |
Air-cooled (7.5–132 kW); water-cooled (75–400 kW); customer-specified |
| Oil Carry-Over |
≤3 ppm (after integrated separator); ≤0.01 ppm with downstream coalescing filter |
| Discharge Temperature |
≤ambient + 10°C after aftercooler (air-cooled); ≤40°C (water-cooled) |
| Duty Cycle |
100% continuous; no mandatory rest periods |
| Controller |
PLC with touchscreen HMI; RS-485 / Modbus RTU remote interface standard |
| Protection Class |
IP54 standard; IP55 / IP65 option |
| Certification |
GOST-R; ISO 1217 (FAD); CE marking available on request |
How the Screw Compressor Works
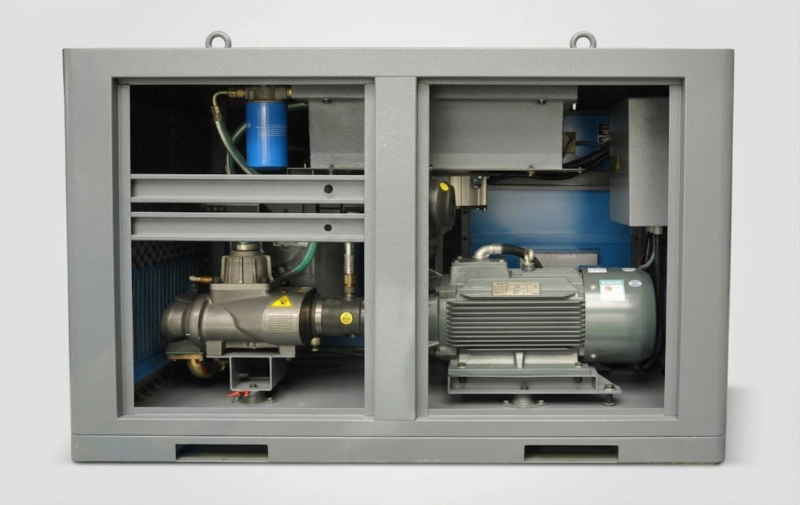
The screw compressor operates with a pair of intermeshing helical rotors — a four-lobe male rotor and a six-groove female rotor — rotating in opposite directions inside a precision-machined housing. Air enters at the suction end and is trapped in the V-shaped space between the rotor lobes and the housing wall. As the rotors turn, this trapped volume decreases continuously along the rotor length toward the discharge end, compressing the air without the need for suction or discharge valves. The absence of valves is the primary reliability advantage of the screw compressor over a reciprocating machine: valve failure is the most frequent cause of unplanned downtime in reciprocating compressors, and eliminating this failure mode produces a unit that runs continuously for 20,000–40,000 hours between major service interventions.
Oil injection plays a central role in the operating cycle. A controlled quantity of compressor oil is injected into the compression chamber, where it performs three functions simultaneously: it seals the small clearance between the rotor tips and the housing, preventing slip of high-pressure gas back to the suction side and maintaining volumetric efficiency; it lubricates the rotor contact surfaces, eliminating the need for timing gears in most designs; and it absorbs the heat of compression, keeping the discharge gas temperature low enough that a single-stage screw compressor can achieve pressure ratios of up to 13:1 without inter-stage cooling. The oil is separated from the compressed air in the integrated oil separator, cooled in the oil cooler, filtered, and returned to the injection point. The air, now separated from the bulk of the oil, passes through the aftercooler where it is cooled to near-ambient temperature, and residual oil content at the package outlet is typically below 3 ppm.
No Suction or Discharge Valves
The screw compressor achieves compression by rotor geometry alone, without suction or discharge valves. Valve failure — the most common cause of reciprocating compressor downtime — is eliminated. The result is a machine capable of running at 100% load continuously for 20,000–40,000 hours between major overhauls.
Oil-Injection Cooling
Injected oil absorbs the heat of compression inside the screw compressor rotor housing, limiting discharge temperature to 80–100°C before the aftercooler. Single-stage compression to 1.3 MPa without inter-stage cooling or water jackets. The oil is separated, cooled, and recycled continuously within the sealed system.
VFD Speed Control
VFD models vary the screw compressor rotor speed in direct response to network pressure, matching output to actual demand at every moment. Power consumption tracks the load fraction linearly — at 60% demand, the screw compressor uses approximately 60% of full-load power. Fixed-speed compressors at 60% load cycle between full power and idle, consuming 70–80% of full-load power for the same useful output.
Integrated Package
Every screw compressor unit leaves the factory as a fully assembled, tested package: rotors, motor, oil system, separator, aftercooler, inlet filter, safety valve, and PLC controller on a single baseframe. Installation on site requires connection to the electrical supply, the compressed air network, and a cooling water supply (water-cooled models). No inter-component pipework assembly on site.
Screw Compressor Application Scenarios
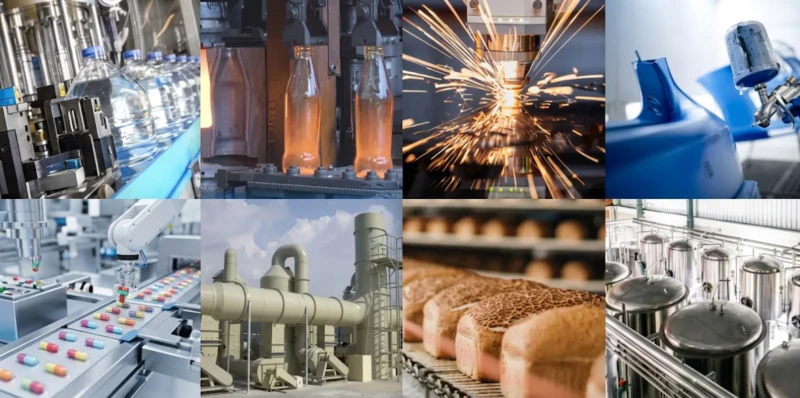
🏭Metal Fabrication and Machining — Pneumatic Tools and CNC Clamping
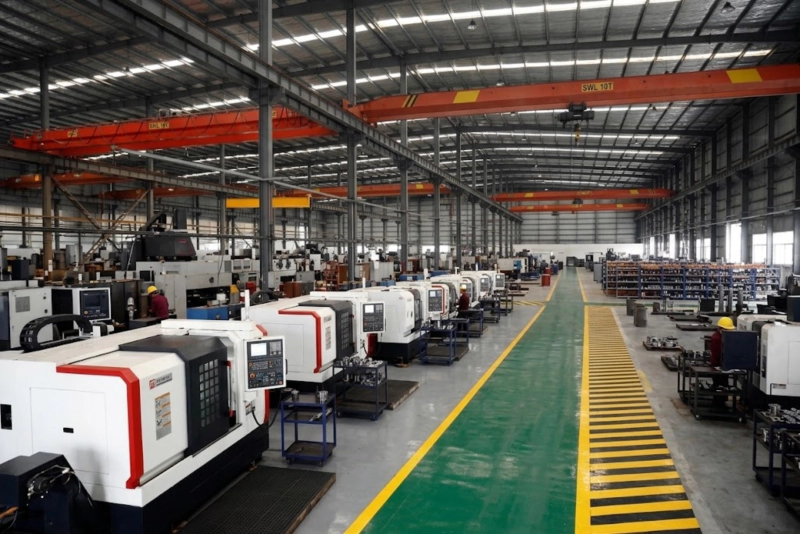
Metal fabrication workshops and CNC machining centres use compressed air continuously for pneumatic tools (grinders, drills, riveters, impact wrenches), CNC workholding and clamping circuits, chip blowing at cutting stations, and coolant mist systems. Demand is variable but rarely drops to zero during production hours — the VFD screw compressor is the standard specification for these workshops. A 37–75 kW screw compressor at 0.8 MPa covers most medium-scale machining centres, with 90–160 kW models serving large fabrication halls with multiple simultaneous pneumatic tool users. The continuous duty rating of the screw compressor and the low noise level compared to a reciprocating machine are additional practical advantages in production workshop environments.
🍠Food and Beverage Processing — Packaging, Conveying and Cleaning
Food and beverage plants use compressed air for product conveying, filling machine actuation, packaging and sealing machinery, bottle blowing pre-forms, and equipment cleaning. Food contact applications require air meeting ISO 8573-1 Class 1 or Class 2 oil content, which is achieved with a screw compressor package fitted with downstream coalescing and activated carbon filtration — reducing oil carry-over from the standard 3 ppm package outlet to below 0.01 ppm. A 22–55 kW screw compressor unit serves a typical medium-scale food processing line; larger facilities require 75–132 kW models. The fully enclosed screw compressor package with IP54 or IP55 protection is suitable for the washdown environment of food production floors.
💊Pharmaceutical and Chemical — Process Air and Instrument Air
Pharmaceutical plants and chemical facilities use instrument air for pneumatic valve actuators, control systems, and analytical instruments. Instrument air requires a dew point of −40°C or lower (ISO 8573-1 Class 1 moisture) — achieved by passing the screw compressor output through a refrigeration or desiccant air dryer. Process air for tablet coating, fluid bed drying, and spray drying requires high flow rates at 0.4–0.7 MPa. A screw compressor in the 55–110 kW range serves most medium-scale pharmaceutical production lines for instrument air, with larger multi-compressor systems required for process air duties. The VFD screw compressor is specified for pharmaceutical instrument air because the stable network pressure it maintains reduces diaphragm valve wear across the instrument air distribution system.
🏗Construction and Mining — Pneumatic Equipment and Rock Drilling
Construction sites and mining operations use compressed air at 0.7–1.0 MPa for rock drills, jackhammers, shotcrete equipment, and ventilation systems. Portable trailer-mounted screw compressor units in the 30–90 kW range provide the mobile compressed air supply for these applications. Stationary screw compressor installations serve precast concrete production facilities and quarry operations where demand is continuous and high. For rock drilling applications requiring 1.0–1.3 MPa, the screw compressor 1.0 MPa and 1.3 MPa pressure variants cover the specification without the need for a booster stage.
Screw Compressor: Core Advantages
⏰
Continuous Duty — No Cycling, No Downtime
The unit operates at 100% load continuously without mandatory rest periods or cool-down cycles. The absence of valves, piston rings, and reciprocating masses means the machine is not subject to the fatigue-driven maintenance intervals that limit reciprocating compressor run time. A well-maintained machine runs 20,000–40,000 hours between major overhauls — 3–5 years of continuous service before the rotor housing clearances require attention.
⚡
VFD Energy Saving — Up to 35% Lower Annual Cost
VFD models match motor speed to demand in real time, consuming power proportional to actual air flow. In facilities with average demand at 60–80% of installed capacity — which describes most manufacturing plants — this reduces annual energy cost by 20–35% compared with an equivalent fixed-speed machine on the same load profile. Energy cost represents 70–80% of a screw compressor lifetime cost; a 25% energy reduction over a 10-year service life pays for the VFD premium many times over.
🔈
Low Noise — 65–78 dB(A) at 1 Metre
Noise output is 65–78 dB(A) at 1 metre depending on model size — substantially lower than a reciprocating compressor of equivalent capacity, which typically produces 80–90 dB(A). This allows the unit to be installed in or adjacent to production areas without acoustic enclosures, and does not require hearing protection for personnel working near the machine during normal operation in most installation configurations.
📈
Stable Discharge Pressure
The continuous rotary compression produces an essentially pulsation-free discharge pressure without the cyclic pressure variation of a reciprocating machine. Downstream pressure is held within ±0.02 MPa of setpoint by the PLC pressure control system, maintaining consistent operating conditions for pneumatic actuators, CNC clamping circuits, and instrument air consumers that are sensitive to pressure fluctuation.
📄
Simple Maintenance Schedule
Annual service covers: air filter replacement (2,000–4,000 hours); oil separator element replacement (4,000–8,000 hours); compressor oil change (4,000–8,000 hours); oil filter replacement (2,000–4,000 hours); belt inspection and tensioning if applicable; and controller sensor calibration. All consumable items are accessible from the front of the package without removing the unit from its installation position. Spare parts are stocked in Russia for 24–72 hour dispatch.
🕑
Fast Delivery and Local Support
Standard screw compressor models in the 7.5–132 kW range are available from stock or with 2–6 week delivery from our Russian distribution network. Larger models (160–400 kW) have 6–12 week delivery. After-sales support, consumable spare parts, and service personnel are available across Russia. GOST-R certification and Russian-language documentation are included as standard with every screw compressor unit.
Screw Compressor vs. Reciprocating Compressor for Industrial Air Supply
Note: The following comparison is provided for general guidance. The appropriate compressor type depends on the specific application, duty cycle, and site conditions. Contact our engineering team to discuss the correct selection for your requirements.
| Factor |
Screw Compressor |
Reciprocating Compressor |
| Duty cycle |
100% continuous |
Typically 60–80% |
| Noise level (75 kW) |
≤72 dB(A) |
80–88 dB(A) |
| Vibration |
Low; no isolation pads required |
Higher; anti-vibration mounts standard |
| Part-load efficiency (VFD) |
Excellent; linear power–flow |
Moderate; unloader cycling |
| Pressure pulsation |
Near-zero |
Inherent; pulsation dampener required |
| Max pressure (single stage) |
1.3 MPa |
Up to 30+ MPa |
| Service interval |
4,000–8,000 h (oil change) |
2,000–3,000 h (oil and valves) |
| Best application |
General industrial air; continuous medium pressure |
High pressure; special gas; low duty cycle |
FAQ — Screw Compressor
Q1: How do I choose between a fixed-speed and VFD screw compressor?
If your facility air demand is consistent and close to the compressor rated capacity for most of the operating day — for example, a production line that runs at near-constant output during shifts — a fixed-speed screw compressor is the lower-cost choice. If demand varies significantly during the day, week, or season — as is the case in most fabrication shops, food processing plants, and facilities with multiple shift patterns — a VFD unit will reduce annual energy cost by 20–35% and pay back its price premium in 18–36 months. Our engineering team can perform a load analysis to quantify the payback for your specific installation.
Q2: What downstream equipment does a screw compressor require?
The package includes the aftercooler and integrated oil separator as standard, bringing oil carry-over to below 3 ppm and air temperature to near-ambient at the package outlet. For most general industrial compressed air applications, a drain valve and distribution pipework are the only additional requirements. For applications requiring lower oil content — food contact air, pharmaceutical process air, instrument air — a downstream coalescing filter and activated carbon filter bring the air to ISO 8573-1 Class 1 oil specification. For low dew point instrument air, a refrigeration or desiccant dryer is required downstream.
Q3: How do I size a screw compressor for my facility?
Screw compressor sizing requires two primary inputs: total connected air demand (the sum of all pneumatic tool and equipment consumption at rated conditions, in m³/min) and the required network pressure (in MPa or bar). From these, apply a demand diversity factor — typically 0.5–0.7 for manufacturing facilities, reflecting that not all tools operate simultaneously — to arrive at the design FAD. Then add 10–15% margin for future capacity and unforeseen demand growth. For example: 20 pneumatic tools at 0.020 m³/min each = 0.40 m³/min total, at 0.7 diversity = 0.28 m³/min design demand, at 0.8 MPa. The SC-15A (0.8 MPa FAD of 1.8 m³/min at 15 kW) would be the appropriate screw compressor selection for this example, with reserve capacity for growth. Our engineering team can assist with demand surveys and screw compressor sizing at no cost for serious enquiries.
Q4: What maintenance does a screw compressor require and how often?
Routine screw compressor maintenance: air filter replacement every 2,000–4,000 hours or annually, whichever is sooner; oil filter and separator element replacement every 4,000–8,000 hours; compressor oil change every 4,000–8,000 hours (food-grade or synthetic oil extends this interval); V-belt inspection and tensioning every 2,000 hours where applicable; and controller sensor and pressure transducer calibration check annually. Major overhaul — rotor clearance inspection and bearing replacement — is typically required at 20,000–40,000 hours depending on operating conditions. Total annual maintenance cost for a 37 kW screw compressor is typically less than 2% of the machine purchase price in consumable parts and service time.
Q5: What is the expected service life of a screw compressor?
A well-maintained screw compressor operating within its rated conditions typically reaches 60,000–100,000 hours of total service life before the rotor housing and bearing components require replacement at a cost that makes replacement of the complete unit more economical. At 8,000 hours per year (a two-shift, six-day-a-week operation), this represents 7–12 years of service. The primary factors that shorten screw compressor service life below this range are operating with a clogged inlet filter (increases rotor differential pressure and bearing load), running with contaminated oil or beyond oil change intervals (accelerates rotor tip and housing wear), and running at consistently elevated discharge temperature (above 95°C before the aftercooler, indicating cooling system problems).
Q6: What information is needed to request a screw compressor proposal?
To obtain a screw compressor proposal, provide: required FAD in m³/min at the operating pressure; required working pressure (0.7, 0.8, 1.0, or 1.3 MPa); fixed-speed or VFD requirement; air-cooled or water-cooled cooling preference; site electrical supply voltage (380 V or 6 kV); ambient temperature at the installation location; and whether GOST-R documentation is required. For food, pharmaceutical, or instrument air applications, also state the required ISO 8573-1 air quality class so our team can include the appropriate downstream filtration and drying equipment in the package quotation. Response within 24 hours.
Request a Screw Compressor Proposal
Our engineering team supplies screw compressors for industrial compressed air applications across Russia and the CIS. 18 standard models from 7.5 kW to 400 kW; fixed-speed and VFD; air-cooled and water-cooled; GOST-R certified with full Russian-language documentation. Consumable parts stocked in Russia for 24–72 hour dispatch. Standard screw compressor models available from stock or 2–6 week delivery.
Screw Compressor — Technical Enquiry
Get a Screw Compressor Quotation for Your Facility
Compressed air specialists respond to all screw compressor enquiries within 24 hours. GOST-R documentation included.
Request a Quote
Include in Your Screw Compressor Enquiry
✓ Required FAD (m³/min)
✓ Working pressure (0.7 / 0.8 / 1.0 / 1.3 MPa)
✓ Fixed-speed or VFD
✓ Air-cooled or water-cooled
✓ Site electrical supply voltage
✓ Ambient temperature at installation
✓ Air quality requirement (ISO 8573-1 class)
✓ Required delivery date