Technical Knowledge · GOST Standard · Oxygen Safety · Compressor Specification · Russia
GOST 12.2.052 is the Russian national standard that governs the safety of equipment working with gaseous oxygen. It establishes the materials, design features, cleanliness requirements, and operating limits that apply to oxygen compressors, pipework, fittings, and pressure vessels in Russian industrial installations. Understanding this standard is essential for specifying oxygen compressors, commissioning oxygen systems, and operating oxygen equipment safely in Russia and the CIS. This guide explains the key requirements of GOST 12.2.052 as they apply specifically to oxygen compressors and their installation.
✓ Materials Restrictions
✓ Degreasing Standards
✓ ZW / DW / LW Series
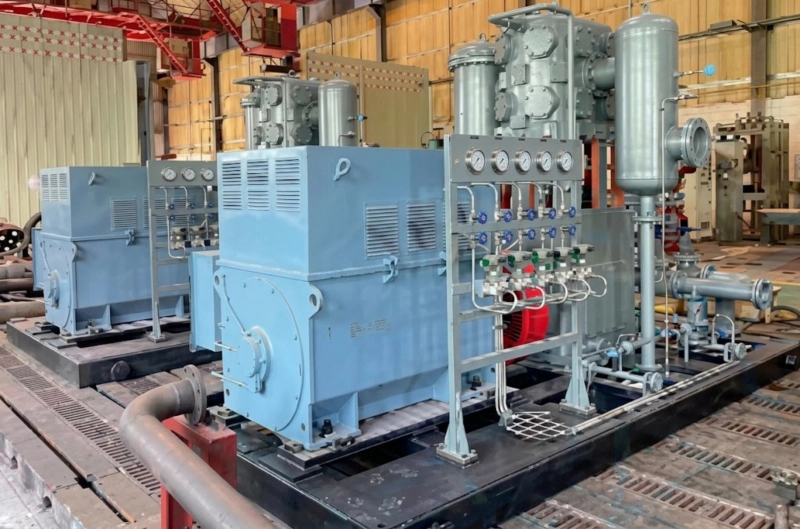
Oil-free oxygen compressor in service — all oxygen-wetted components degreased to below 50 mg/m² hydrocarbon residue per GOST 12.2.052, copper-free construction throughout, PTFE self-lubricating piston rings, labyrinth distance piece preventing crankcase oil migration. Every compressor in oxygen service at any pressure above 0.5 MPa must comply with GOST 12.2.052 material and design requirements.
What GOST 12.2.052 Covers and Why It Exists
GOST 12.2.052 — «Occupational Safety Standards System. Equipment Working with Gaseous Oxygen. Safety Requirements» — was developed to address the specific ignition and combustion hazards that arise when hydrocarbon materials contact gaseous oxygen at elevated pressure. Unlike nitrogen, argon, and other inert gases, oxygen actively supports combustion: materials that do not normally burn in air can ignite and burn in oxygen at much lower temperatures and pressures, and materials that smoulder or char in air may burn vigorously or even detonate in oxygen. The standard systematically addresses each pathway by which a hydrocarbon ignition source can reach the oxygen stream in an industrial compression and distribution system.
The standard applies to all equipment that works with gaseous oxygen at pressures above 0.5 MPa (5 bar), including: reciprocating and centrifugal oxygen compressors; oxygen distribution pipework and fittings; pressure vessels containing gaseous oxygen; oxygen pressure regulators and control valves; and all accessories (filters, moisture separators, safety valves, instrumentation) in the oxygen stream. Equipment operating below 0.5 MPa — such as low-pressure oxygen lines in hospitals or welding supply at near-atmospheric pressure — is not covered by GOST 12.2.052, though other Russian standards apply.
Key Requirement 1: Prohibition of Hydrocarbon Lubricants
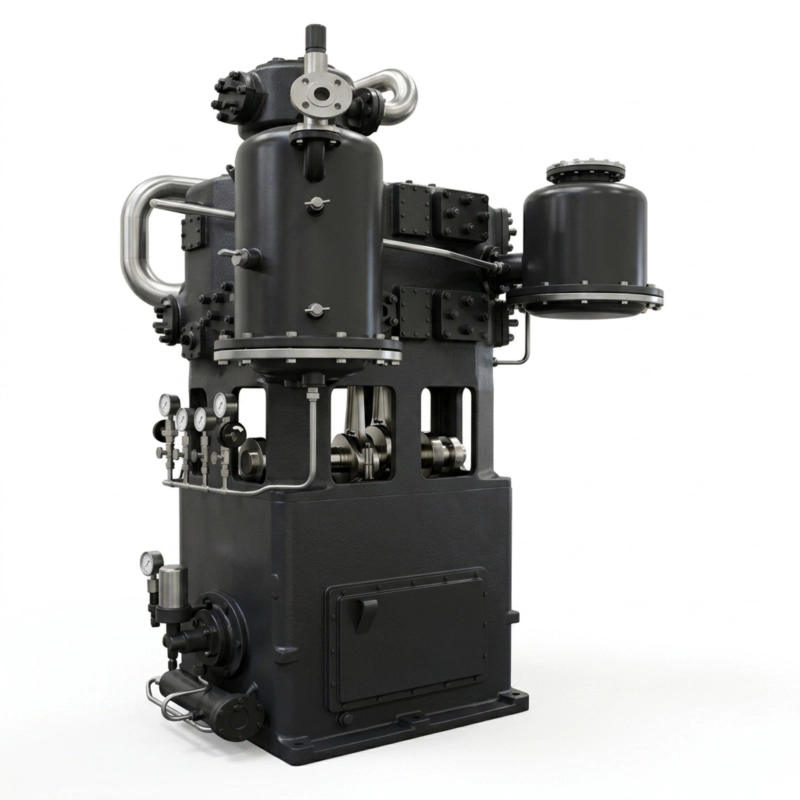
The most fundamental requirement of GOST 12.2.052 for oxygen compressors is the prohibition of hydrocarbon lubricants in the oxygen compression space at pressures above 0.5 MPa. This prohibition exists because mineral oils and synthetic hydrocarbon lubricants can ignite in high-pressure oxygen at temperatures far below their flash point in air. The adiabatic compression heating of gas trapped in a small volume — such as a compressor valve seat opening event or a rapid valve closure — can momentarily reach temperatures sufficient to ignite hydrocarbon oil in oxygen even when the bulk gas temperature remains well below the oil’s normal ignition temperature. This mechanism is known as diesel effect ignition and has been responsible for multiple oxygen compressor fires in Russia and internationally.
To comply with this prohibition, the oxygen compressor must use an oil-free cylinder design in which no hydrocarbon lubricant contacts the oxygen gas stream. The ZW, DW, and LW series oxygen compressors achieve this through PTFE self-lubricating piston rings (which require no oil at the ring-bore interface) and a labyrinth distance piece between the cylinder and the crankcase that prevents crankcase oil from migrating along the piston rod into the compression space. The crankcase lubrication oil — which is still present to lubricate the crankshaft bearings, connecting rod bearings, and crosshead guides — never contacts the oxygen gas stream.
Safety Requirement
The use of any hydrocarbon lubricant in contact with the oxygen gas stream at pressures above 0.5 MPa is prohibited by GOST 12.2.052 and constitutes a fire and explosion hazard. This prohibition applies to both the compression cylinder and all downstream oxygen pipework, fittings, and instruments. A compressor that drips crankcase oil into the oxygen stream does not meet GOST 12.2.052 regardless of the presence of downstream oil filters — the prohibition is on contact, not on carry-over above a detection limit. There is no engineering workaround to this requirement: only the oil-free cylinder design complies.
Key Requirement 2: Copper-Free Wetted Components
GOST 12.2.052 prohibits the use of copper, brass, and bronze in all components in contact with gaseous oxygen at pressures above 0.5 MPa. The prohibition on copper and copper alloys in oxygen service has two separate engineering bases:
Copper acts as a catalyst for the oxidation of any hydrocarbon residue present on oxygen-wetted surfaces. Even a trace of hydrocarbon contamination on a copper or brass surface — below the level detectable by the standard degreasing verification test — can be catalytically oxidised by oxygen at pressures above 0.5 MPa at temperatures significantly below the normal ignition temperature. This catalytic pathway lowers the effective ignition threshold of hydrocarbon contamination in oxygen contact with copper surfaces to a level where normal degreasing practices cannot guarantee safety.
Copper oxide (CuO), which forms on copper surfaces in oxygen service, is particularly sensitive to impact ignition. A particle of copper oxide accelerated by high-pressure oxygen flow — in a valve closure event or a sudden pressure change — and impacting a downstream surface can generate sufficient local heating to ignite oxygen-compatible materials at that contact point. The prohibition on copper in oxygen pipework and fittings eliminates this particle generation mechanism.
In practice, the copper-free requirement means that all oxygen compressor cylinders, valve bodies, valve seats, piston rods, inter-stage cooler tubes and headers, aftercooler, moisture separator vessels, safety valve bodies, and all pipework and fittings in the oxygen stream use carbon steel, stainless steel, or aluminium alloys. Stainless steel is preferred for high-pressure oxygen pipework above 10 MPa because of its higher tensile strength and lower contamination risk compared with carbon steel. All gasket and seal materials in oxygen service must also comply — PTFE, non-asbestos fibre, and spiral-wound stainless steel gaskets are acceptable; copper-spiral or soft copper gaskets are prohibited.
Key Requirement 3: Degreasing to Below 50 mg/m²
GOST 12.2.052 specifies that all oxygen-wetted surfaces of compressors, pipework, and fittings must be degreased before assembly and before commissioning, with the residual hydrocarbon contamination level verified to be below 50 mg/m² of surface area (50 milligrams per square metre, equivalent to approximately 0.5 mg per 100 cm²). This is a very low contamination level — equivalent to a monomolecular layer of oil spread very thinly across the surface — and achieving it requires specific degreasing procedures rather than simple cleaning.
The standard GOST 12.2.052 degreasing procedure for oxygen compressor components involves: initial mechanical cleaning to remove loose scale, rust, and weld spatter; chemical degreasing using a suitable solvent (trichloroethylene or similar chlorinated solvent, or an aqueous alkaline degreasing solution) applied by immersion or flushing; rinsing with clean water or solvent to remove the degreasing agent; drying with clean oil-free nitrogen or filtered dry air; verification of residual contamination level using a wipe test and UV lamp inspection (organic contamination fluoresces under UV); and reassembly in a clean environment without reintroducing contamination. All components are reassembled with clean cotton gloves and oil-free tools; no petroleum-based thread compounds are used on oxygen-side fastener threads.
Key Requirement 4: Discharge Temperature Limit
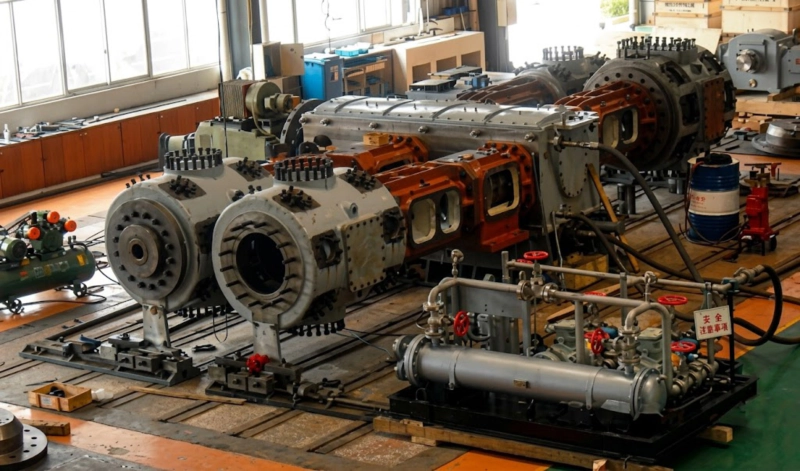
GOST 12.2.052 establishes a maximum discharge temperature of 140°C for oxygen compressors. This limit exists because at temperatures above 140°C, the rate at which even trace hydrocarbon contamination — from PTFE ring wear particles, seal degradation products, or residual contamination from imperfect degreasing — can be oxidised by the oxygen stream increases to a level where the risk of a self-sustaining oxidation reaction becomes non-negligible. Below 140°C, the oxidation kinetics are slow enough that any trace contamination present is oxidised gradually and safely; above 140°C, the oxidation rate increases rapidly with temperature.
The 140°C discharge temperature limit is enforced in the compressor installation by a high-temperature trip that shuts the compressor down automatically if any stage discharge temperature exceeds the limit. The trip setpoint is typically 135°C (5°C below the GOST limit) to allow for sensor measurement uncertainty and to provide a warning margin before the safety limit is reached. A temperature alarm at 125°C alerts the operator to investigate the cause before the automatic trip activates. The causes of rising discharge temperature in an oil-free oxygen compressor are: worn piston rings (increased internal leakage re-compression), reduced inter-stage cooling water flow, elevated cooling water temperature, or partial suction valve failure.
| GOST 12.2.052 Requirement | Parameter / Limit | ZW/DW/LW Compliance |
|---|---|---|
| No hydrocarbon lubricant in O₂ stream | Mandatory above 0.5 MPa | PTFE rings + labyrinth distance piece |
| Copper-free wetted components | All components above 0.5 MPa | Carbon steel / stainless steel throughout |
| Degreasing at factory | < 50 mg/m² residual HC | Documented akt obezzhirivaniya supplied |
| Maximum discharge temperature | 140°C per stage | 135°C auto-trip; 125°C alarm standard |
| No prohibited ring materials | No carbon/graphite/bronze fill in rings | Virgin PTFE rings supplied as standard |
| Safety valve and instrumentation | Rated for O₂ service; copper-free | Carbon/stainless steel; O₂-rated seals |
Compliance summary for ZW, DW, and LW series oxygen compressors. Full compliance documentation (GOST-R certificate, akt obezzhirivaniya, material certificates for all oxygen-wetted components, equipment passport) is supplied with every compressor ordered for oxygen service.
Cleanliness Standards in ISBM: ISO 8573-1 vs GOST 12.2.052
The GOST 12.2.052 degreasing limit of 50 mg/m² for oxygen equipment surfaces has a conceptual parallel in the ISO 8573-1 Class 1 oil content limit of 0.01 mg/m³ for food-contact compressed air used in injection stretch blow moulding (ISBM) production. Both standards address the same fundamental concern: hydrocarbon contamination must be eliminated from a process stream that contacts either an extremely reactive gas (oxygen) or a food-contact surface (the PET bottle interior). GOST 12.2.052 controls surface contamination of solid components; ISO 8573-1 controls contamination in the gas stream itself. Both require a combination of oil-free design (no source of contamination) and verification testing (degreasing record or compressed air quality analysis) to demonstrate compliance. The engineering discipline of eliminating contamination at the source — rather than filtering it downstream — is common to both standards.
FAQ — GOST 12.2.052 Oxygen Equipment Safety
GOST 12.2.052 Compliant Oxygen Compressors
ZW, DW, and LW series oil-free oxygen compressors supplied with full GOST 12.2.052 compliance documentation — GOST-R certificate, equipment passport, material certificates, factory degreasing record, and acceptance test record. All in Russian language. Response within 48 hours.